Contract Manufacturing for Injection Molded Plastic Products in North America
(800) 824.0607
The 2026 carbon fiber market will reward stable production, not impressive brochures. A modern Carbon fiber production line factory must control precursor quality, oxidation, carbonization, surface treatment, and winding accuracy. Each stage affects tensile strength, modulus, yield, and energy consumption. Small temperature changes can alter the final tow. That detail matters.
Dr. Akio Shindo, a pioneer of PAN-based carbon fiber development, emphasized a lasting production principle: “Stable processing is essential for consistent carbon fiber quality.” His work reminds buyers that equipment design cannot replace process discipline. Leading manufacturers should demonstrate furnace uniformity, tension control, atmosphere management, and reliable line integration. They should also provide traceable testing data. Claims without production evidence deserve caution.
This review examines the top carbon fiber production line manufacturers expected to influence 2026. It considers engineering experience, automation depth, maintenance support, energy performance, and customization capability. Practical evidence matters more than polished marketing. A strong supplier should explain commissioning procedures and failure-response plans. It should also show how the line performs during long, continuous runs.
Not every high-speed line delivers better economics. That assumption can fail. Excessive speed may increase breaks, scrap, or unstable surface treatment. Buyers should compare usable output, not only rated capacity. They should inspect factory references, sample fiber data, spare-parts access, and operator training. Regional service coverage may become decisive. This guide therefore balances technical performance with commercial reliability, while acknowledging one uncomfortable truth: even advanced lines require skilled people, careful calibration, and ongoing improvement.
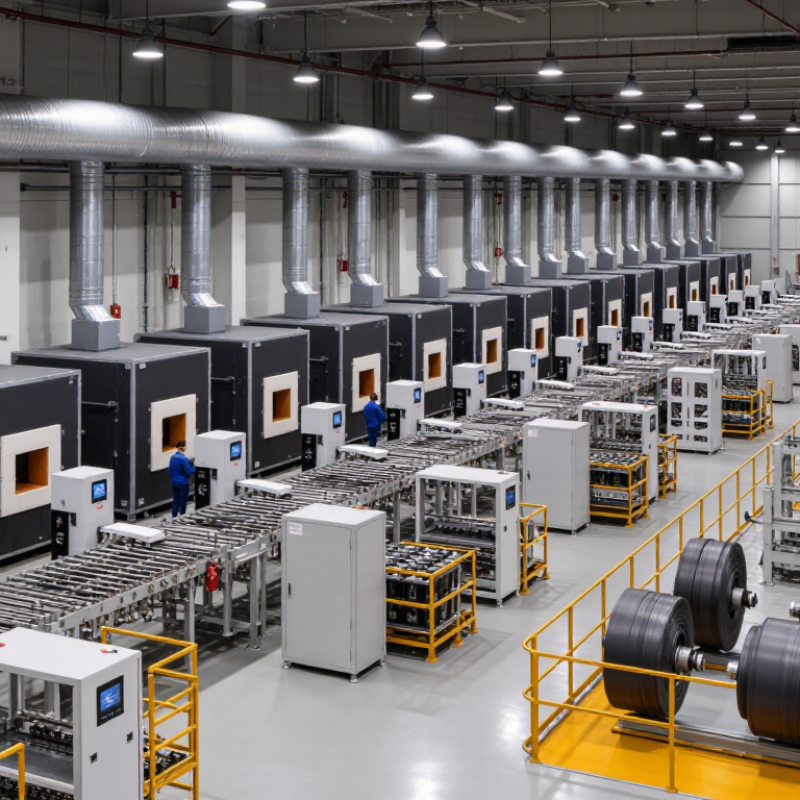
A carbon fiber production line is an integrated industrial system that converts polymer precursor into strong, lightweight carbon fiber. In practical plant work, the line feels less like one machine and more like a carefully timed chain. It typically includes precursor unwinding, stabilization ovens, carbonization furnaces, surface treatment, sizing, drying, and final winding. Each section changes the filament gradually. The fiber may look unchanged to the eye. Inside, its molecular structure is becoming more heat-resistant and ordered.
During stabilization, controlled heat and airflow prevent the precursor from melting. Carbonization then removes non-carbon elements in oxygen-limited furnaces. Temperatures can exceed 1,000°C, so furnace sealing and gas monitoring matter greatly. Line speed, tension, residence time, and temperature must remain coordinated. A small tension drift can create fuzz, breaks, or uneven tow packages. Operators inspect fiber surfaces, check tensile samples, and compare furnace data with production records. That part matters. These details reveal whether the process is stable, not merely whether the line is running.
A reliable line also needs alarms, interlocks, exhaust treatment, calibration routines, and traceable quality records. Surface treatment improves bonding with resins, while sizing protects filaments during handling. The design depends on tow size, target strength, energy use, and required output. No line is perfect. In my view, early trials often expose overlooked heat loss or difficult maintenance access. Those findings should change the layout before full-scale production begins. A polished specification can still hide practical weaknesses.
A carbon fiber production line converts a precursor, commonly PAN or pitch, into carbon fiber through controlled preparation, stabilization, carbonization, optional graphitization, surface treatment, and sizing. The chart shows typical industrial temperature ranges for the main thermal and finishing stages. Actual settings vary according to precursor type, fiber grade, tow size, and required mechanical properties.
2026 Top Carbon Fiber Production Line Manufacturers?
Key Stages of Carbon Fiber Manufacturing
Carbon fiber production begins with precursor preparation, usually using carefully controlled polymer fibers. Operators inspect fiber uniformity, moisture, and tension before oxidation starts. Small variations can affect the final tensile strength. The stabilization stage heats the fibers in air, often through several temperature zones. This process removes unwanted elements and forms a stable molecular structure. It requires patience.
Carbonization follows in an oxygen-limited furnace. Temperatures may rise above 1,000°C, depending on the required fiber grade. The line must control furnace pressure, residence time, and fiber speed together. Surface treatment then improves bonding between the fiber and resin. A sizing layer protects the filaments during handling and later processing. Final winding, testing, and packaging complete the production route. In practice, defects often appear earlier than expected. That makes traceability essential.
Tips: Keep tension sensors calibrated and record every heating-zone change. Inspect broken filaments under magnification, not only through automated alarms. Do not treat higher furnace temperatures as an automatic quality improvement. Energy use, maintenance intervals, and line stability also deserve attention. A reliable manufacturer should provide process data, trial results, safety documentation, and realistic performance limits. Some production plans look efficient on paper but need adjustment after pilot runs.
Manufacturer-neutral production-line benchmark based on commonly used PAN-based carbon fiber processing conditions
| Production Stage | Primary Material or Input | Typical Operating Conditions | Core Equipment | Key Process-Control Variables | Typical Output or Conversion | Quality-Control Focus | Production-Line Selection Criteria |
|---|---|---|---|---|---|---|---|
| 1. Precursor Preparation | Acrylonitrile-based polymer, commonly PAN, converted into precursor dope and wet- or dry-spun filaments | Polymerization and spinning conditions vary according to polymer composition, solvent system, spinneret design, and target filament count | Polymerization vessels, dope tanks, metering pumps, spinnerets, coagulation baths, washing units, and drawing rolls | Polymer molecular weight, solution viscosity, spinning speed, draw ratio, filament linear density, and impurity level | Continuous PAN precursor tow with controlled filament count and orientation | Filament uniformity, tensile strength, elongation, denier, surface defects, and residual solvent | Stable metering, precise tension control, effective solvent recovery, and compatibility with the intended tow size |
| 2. Precursor Washing and Drying | Freshly spun PAN precursor containing residual solvent, water, and processing additives | Multiple washing and drying zones; exact temperature and residence time depend on solvent chemistry and line speed | Counter-current washing units, squeeze rolls, drying ovens, air knives, and tension-control systems | Residual solvent, moisture content, tow spread, drying temperature, line tension, and residence time | Clean, dry, and dimensionally stable precursor tow | Residual solvent, moisture uniformity, filament bonding, fuzz generation, and tow-width consistency | Low-tension conveying, uniform drying across the tow width, and closed-loop solvent or water management |
| 3. Stabilization or Oxidation | Dry PAN precursor tow | Typically approximately 200–300 °C in an oxidizing atmosphere; the tow is heated gradually to prevent runaway exothermic reactions | Multi-zone stabilization ovens, air-circulation systems, tow guides, exhaust treatment, and temperature-control systems | Temperature profile, oxygen availability, residence time, tow tension, oven uniformity, and exotherm control | Infusible, thermally stabilized PAN fiber with a ladder-like molecular structure | Stabilization index, density, shrinkage, color uniformity, tensile retention, and cross-sectional consistency | Independent zone control, reliable exhaust handling, even airflow, fire protection, and accurate tension regulation |
| 4. Low-Temperature Carbonization | Stabilized PAN fiber | Usually about 800–1,000 °C in an inert atmosphere such as nitrogen | Inert-atmosphere carbonization furnaces, gas-sealing systems, high-temperature rolls, cooling sections, and off-gas treatment | Furnace temperature, nitrogen flow and purity, residence time, line tension, furnace pressure, and off-gas composition | Carbon fiber with increased carbon content and reduced non-carbon elements | Tensile strength, modulus, density, electrical resistivity, tow integrity, and surface cleanliness | Uniform heat distribution, controlled oxygen exclusion, low tow breakage, efficient inert-gas use, and safe off-gas handling |
| 5. High-Temperature Carbonization | Partially carbonized fiber | Commonly approximately 1,200–1,600 °C under inert conditions, depending on the required fiber grade | High-temperature furnaces, graphite or ceramic hot zones, inert-gas systems, tension stands, and cooling chambers | Peak temperature, temperature uniformity, gas purity, tow tension, residence time, and furnace atmosphere | High-strength carbon fiber with a more developed turbostratic carbon structure | Strength, modulus, density, filament breaks, fuzz level, electrical resistance, and batch consistency | Stable high-temperature operation, low contamination, precise tension control, heat recovery, and maintainable hot-zone components |
| 6. Graphitization, When Required | Carbonized fiber intended for high-modulus or specialized grades | Approximately 2,000–3,000 °C in an inert atmosphere; not required for every carbon-fiber product | Graphitization furnace, graphite hot zone, inert-gas purification, high-temperature power supply, and cooling system | Maximum temperature, residence time, fiber tension, gas purity, electrical power stability, and hot-zone condition | Higher-modulus carbon fiber with increased graphitic ordering | Modulus, tensile strength, density, electrical conductivity, structural uniformity, and surface condition | High-temperature capability, power efficiency, hot-zone service life, precise tow handling, and contamination control |
| 7. Electrochemical or Controlled Surface Treatment | Carbonized or graphitized fiber | Aqueous electrochemical treatment is commonly used; current density, bath chemistry, and treatment time are product-specific | Electrochemical cells, electrolyte circulation, anodes and cathodes, washing units, conductivity meters, and drying sections | Surface-treatment intensity, bath concentration, pH, conductivity, temperature, residence time, and tow tension | Fiber surface with improved compatibility and interfacial bonding with a selected resin system | Surface oxygen functionality, wettability, interfacial shear strength, tensile retention, and treatment uniformity | Uniform treatment across the tow, accurate bath control, low fiber damage, wastewater management, and resin-specific compatibility |
| 8. Washing and Drying After Treatment | Surface-treated carbon fiber containing residual electrolyte and moisture | Controlled rinsing followed by drying at a temperature that avoids fiber damage and excessive finish degradation | Rinsing tanks, dewatering rolls, dryers, conductivity sensors, wastewater-treatment equipment, and tension controls | Rinse-water conductivity, residual ions, moisture, drying temperature, tow spread, and line tension | Clean, dry, surface-treated carbon fiber ready for sizing | Residual ionic contamination, moisture, surface energy, filament cohesion, and mechanical-property retention | Efficient water use, stable rinse quality, closed-loop monitoring, and minimal tow abrasion |
| 9. Sizing Application | Carbon fiber and a resin-compatible sizing formulation, often aqueous or solvent-based | Application concentration and drying conditions are matched to the target matrix resin and end use | Immersion or kiss-coater, sizing bath, metering rolls, drying oven, circulation system, and concentration-control equipment | Sizing add-on level, bath concentration, viscosity, temperature, pickup uniformity, and drying profile | Carbon fiber with improved handling, filament protection, and matrix-resin compatibility | Sizing percentage, uniformity, fuzz, tensile strength, interfacial performance, and resin wet-out | Accurate low-add-on application, formulation flexibility, clean bath circulation, and repeatable drying |
| 10. Spreading, Winding, and Packaging | Finished sized carbon-fiber tow | Controlled winding tension and package density; packaging format depends on tow size and customer process requirements | Tow spreaders, tension controllers, traversing winders, package-build systems, weighing equipment, and protective packaging stations | Winding tension, package width, winding speed, package density, tow alignment, and splice frequency | Commercial packages such as continuous tow, bobbins, or larger industrial packages | Package geometry, net weight, tow continuity, fuzz, winding defects, labeling, and traceability | Low-tension handling, accurate package formation, automated inspection, barcode traceability, and flexible packaging formats |
| 11. Final Inspection and Release | Packaged carbon-fiber product | Testing follows internal specifications and applicable customer or international methods | Universal testing machines, density and electrical-resistance instruments, microscopy, sizing-analysis equipment, and laboratory data systems | Tensile strength, tensile modulus, elongation, density, sizing content, electrical resistance, and visual quality | Released product with a documented certificate of analysis and production traceability | Lot-to-lot consistency, statistical process control, defect rate, test repeatability, and customer-specification compliance | Integrated laboratory information systems, calibrated instruments, sampling discipline, and complete batch genealogy |
| Technical note: Operating ranges are representative industry values for PAN-based carbon fiber and are not universal set points. Actual conditions depend on precursor chemistry, tow size, target strength and modulus, furnace design, resin system, and applicable product specifications. | |||||||
Evaluating carbon fiber production line manufacturers requires more than comparing machine prices. In plant reviews, I examine precursor compatibility, tow size, furnace temperature control, line speed, and fiber yield. The Global Wind Energy Council’s Global Wind Report 2024 recorded 117 GW of new wind capacity in 2023. This supports continued demand for lightweight composite materials, but demand alone does not prove a supplier’s capability.
A reliable manufacturer should provide pilot-line trials, process data, energy-use measurements, and batch traceability. Ask for tensile strength, modulus, sizing consistency, and defect rates from comparable lines. The International Energy Agency’s Energy Technology Perspectives 2024 highlights resilient supply chains and efficient material production as key industrial priorities. Therefore, evaluate local technical support, spare-parts availability, operator training, and cybersecurity controls. A polished factory tour can mislead. Real production records matter more.
Tips: Request a sample production run using your own precursor. Check whether reported yield includes startup waste. Review acceptance criteria before signing. ISO 9001 and ISO 14001 certifications can support quality and environmental management, but certificates cannot replace technical evidence. I also compare warranty terms with the manufacturer’s commissioning history. No scorecard is perfect. A supplier may offer excellent equipment yet lack practical furnace expertise, and that weakness often appears only after continuous operation begins.
The 2026 market favors production line manufacturers with complete, stable process control. A carbon fiber line must manage oxidation, carbonization, graphitization, surface treatment, sizing, and winding. Each stage affects tensile strength, modulus, yield, and energy consumption. MarketsandMarkets projects the global carbon fiber market to reach about USD 6.6 billion by 2029. Its forecast indicates roughly 11% annual growth from 2024 to 2029. This expansion increases demand for scalable and energy-efficient production equipment.
Leading manufacturers should provide more than furnaces and control cabinets. They need validated temperature profiles, tension systems, clean-room compatibility, and reliable data logging. Industry assessments from the International Energy Agency repeatedly identify industrial efficiency as a major emissions priority. Therefore, modern lines should recover heat and reduce nitrogen losses where practical. Operators also need traceability from precursor tow to finished spool. Small errors can become expensive.
Supplier comparisons remain difficult. Public performance figures are not always measured under identical conditions. Some published claims also seem optimistic. Buyers should request factory acceptance data, line-speed records, maintenance histories, and sample testing. A useful benchmark includes consistent fiber quality above 95% yield, although actual results depend on precursor chemistry and process design. The best 2026 manufacturers will combine engineering experience with transparent evidence, responsive service, and adaptable automation. No ranking is perfect. Process fit still matters most.
Carbon fiber production lines are becoming smarter, cleaner, and more flexible. Modern systems connect precursor preparation, oxidation, carbonization, surface treatment, and quality inspection. Sensors now track furnace temperature, tension, oxygen levels, and fiber strength in real time. Digital twins can predict defects before an entire tow becomes waste. That matters.
Microwave-assisted heating and advanced electric furnaces may reduce thermal losses. An Oak Ridge National Laboratory process assessment places conventional carbon fiber production around 183–286 megajoules per kilogram. Stabilization and carbonization remain major energy users. The 2024 JEC Observer reports global carbon fiber demand above 100,000 tonnes annually. This growth increases pressure on production-line efficiency. Automated tension control can improve consistency, but it cannot replace experienced operators. Data can also mislead when sensors drift or sampling remains too limited. That weakness deserves more attention.
Tips: Compare lines by energy use per kilogram, not only rated output. Request trial data from precursor to finished tow. Check furnace uniformity across the full width. Ask for verified carbon-footprint calculations using ISO 14040 principles. Include recycled fiber handling early. It may reduce future retrofit costs. Teams should also test artificial-intelligence controls under unstable feedstock conditions. Perfect factory data rarely exists.