Contract Manufacturing for Injection Molded Plastic Products in North America
(800) 824.0607
Choosing the right Standard Conveyor in 2026 starts with the product, not a brochure. A carton of dry components behaves differently from a damp, abrasive load or a delicate finished item. Measure typical and maximum loads, then record package dimensions, spacing, speed, and daily operating hours. Small details matter. A belt conveyor may suit continuous movement, while rollers can handle stable cartons between work areas. Inclines, curves, accumulation, and cleaning needs can quickly change the best fit.
Before comparing quotes, map the conveyor’s route and identify how operators will load, inspect, and clear products. Ask suppliers to explain load limits, frame and belt materials, drive access, controls, and maintenance requirements. A catalog rating is only a starting point; confirm that it reflects your actual product and operating conditions. If possible, test representative items on the proposed setup. Watch for slipping, tipping, noisy transfers, or awkward reach points. These observations can reveal problems a drawing misses.
There is no perfect conveyor for every facility. A lower purchase price may bring higher service needs, while extra capacity can add cost without solving a real bottleneck. I would not treat the first specification as final; real products often expose assumptions. Compare options against clear priorities, and document what remains uncertain. That makes the decision easier to review as production needs change.
A standard conveyor is a commonly configured system for moving goods along a fixed route. It usually includes a frame, a belt or rollers, drive components, and basic controls. The exact meaning of “standard” varies by supplier, so check dimensions and load limits rather than relying on the label alone. There is no single design for every task.
In a belt conveyor, a motor turns a drive pulley, pulling the belt around the frame. Rollers support the belt and help keep it aligned.
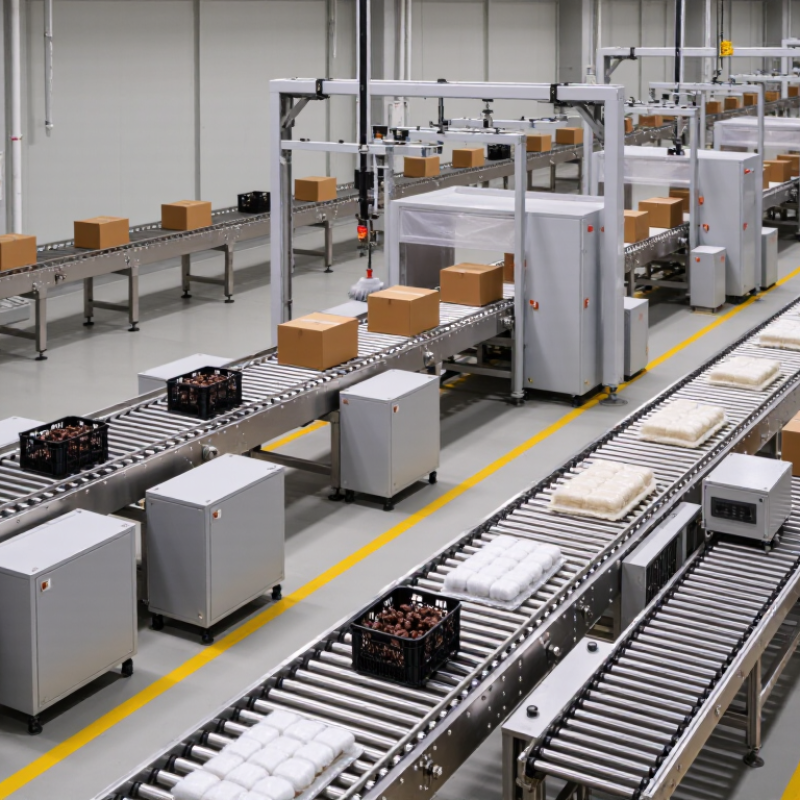
On a roller conveyor, packages move across rotating rollers, either by gravity or powered sections. A carton may travel smoothly until a skewed edge catches at a transfer point.
Small details matter. Match the conveyor to package size, weight, speed, route, and working environment. Dust, moisture, and frequent starts can affect component wear.
Ask how belt tension is adjusted and how operators can access cleaning and maintenance points. A conveyor that fits the layout on paper may still create awkward reaches or bottlenecks on the floor.
Leave room for inspection. Recheck the assumptions.
Choosing the right standard conveyor starts with the material, not the catalogue. Record the smallest and largest item, loaded weight, and contact surface. A smooth carton behaves differently from a soft bag or a tote with a loose base. Note dust, moisture, and temperature too. Small details matter.
Then map real flow. Count average and peak items per minute, not just the daily total. Mark every merge, scan point, handoff, and place where cartons wait. A line designed around average demand may stall during a short rush. For example, watch whether cartons arrive in clusters after packing, and whether operators need room to remove damaged goods. That is often missed.
Walk the proposed route with operators before fixing the layout. Check aisle crossings, maintenance access, noise, and the space needed to clear a jam. I would also test the awkward item, not only the neat sample carton. It is easy to overestimate clean, steady flow. Document assumptions, especially peak rate and accumulation time, so a later change can be traced to its cause. A short trial with actual loads can reveal issues a spreadsheet misses.
A conveyor choice starts with the product, not the catalog. A flat belt suits many cartons and bags, while rollers work well for rigid boxes with stable bases. For heavy loads or rough handling, chain or slat systems may be worth comparing. There is no universal winner. Dust, moisture, temperature, and cleaning routines can change the answer.
Measure the real load range, not just the average box. Record product length, width, weight, and spacing, then compare these figures with belt width and roller pitch. A small carton can snag between widely spaced rollers. That detail is easy to overlook. Check the required speed and hourly volume, too; a faster line may create congestion at packing or inspection stations.
Configuration matters as much as conveyor type. Map every incline, curve, transfer point, and operator access area before choosing a layout. Confirm available floor space and the height of connected equipment. Leave room for maintenance and safe access. A compact design can look efficient on paper, yet be awkward to clean or repair. Recheck assumptions with a site walk-through, because drawings rarely show every obstruction or workflow habit.
In 2026, choose a standard conveyor by checking the work area, not just the product specification. Walk the route during a busy shift. Look for pinch points, emergency-stop access, and space to clear jams safely. The U.S. Bureau of Labor Statistics recorded 2.6 million nonfatal workplace injuries and illnesses in private industry in 2023. That figure is not conveyor-specific, but it makes guarding a design requirement, not an optional extra. Small gaps matter.
Measure floor slope, doorway clearance, and the turning space needed by forklifts. Note dust, washdown routines, temperature changes, and the heaviest loads. A tidy CAD drawing can still miss a floor drain or a hard-to-reach cleanout. I would check those details in person; site notes are easy to get wrong.
Then map how the conveyor will communicate with sensors, controls, and warehouse software. Confirm signal types, operating speeds, and what happens when an upstream machine stops. MHI’s 2024 Annual Industry Report drew on responses from more than 2,000 supply-chain professionals and examines investment in automation and related technologies. Use that context to ask suppliers for a clear integration plan, not just a conveyor layout. Test a realistic product load before final approval. A smooth empty-belt run proves little.
Common nominal belt-width options (mm) provide a starting point for matching the conveyor to the load and available site space.
Choose a width based on the largest load and required spacing, then verify site clearances, guarding and emergency-stop access, and compatibility with upstream and downstream equipment. Width options are common examples, not a substitute for project-specific design or applicable standards.
How to Choose the Right Standard Conveyor in 2026?
A conveyor quote is only comparable when its scope is clear. Check whether it includes supports, guarding, controls, installation, commissioning, and operator training. Ask suppliers to separate equipment price from freight and site work. Then compare expected energy use, routine maintenance, belt or roller replacement, and downtime over the planned service life. A cheap frame can become costly when a jam stops a packing line. Small details matter.
Verify the design against the application, not just a catalogue description. ISO 5048 provides methods for calculating belt conveyor power and tensile forces; ISO 12100 sets out machinery risk-assessment principles. Confirm the applicable editions and local requirements with a qualified engineer. MHI’s 2024 Annual Industry Report found that 55% of surveyed respondents planned to increase supply-chain technology investment. That is useful context, not proof that a particular conveyor will pay back.
Long-term support deserves the same scrutiny as price. Request written warranty terms, spare-parts availability, service response times, and clear escalation contacts. Ask how quickly common wear parts can be shipped, and whether technicians can support your operating hours. Get it in writing. Also check whether the supplier provides maintenance schedules and training materials. These promises can be vague. I would still verify them with customer references and a sample service record before signing.
| Evaluation Area | What to Verify | Evidence or Reference | Practical Acceptance Check |
|---|---|---|---|
| Conveyor type and application | Confirm whether the duty calls for a belt, roller, chain, or other conveyor, based on the load, route, environment, and required transfers. | Layout drawing; product dimensions and weight range; operating sequence; ambient conditions. | The proposed design covers the full product range, incline or decline, transfer points, and access needed for operation and maintenance. |
| Capacity and operating conditions | Specify required throughput, operating hours, loading pattern, conveyor speed, and peak as well as normal demand. | Capacity calculations using the stated product rate, spacing, conveyor speed, and operating schedule. | Calculations state their assumptions and show that the design meets the required rate without relying on unconfirmed future capacity. |
| Dimensions and interfaces | Verify conveyor length, belt or roller width, elevation, transfer height, support locations, and connections to adjacent equipment. | Dimensioned general-arrangement drawing; site measurements; interface and utility schedule. | Drawing dimensions match the site and equipment interfaces; maintenance and emergency access are not obstructed. |
| Purchase and installation cost | Compare the complete installed scope, not only the conveyor equipment price. | Itemized quotation covering equipment, controls, guarding, supports, freight, installation, commissioning, training, taxes, and exclusions. | Each supplier prices the same scope, quantities, site assumptions, and delivery terms; exclusions and change-order rates are identified. |
| Ownership cost | Estimate energy, inspection, routine maintenance, wear parts, downtime, and expected replacement work over the selected evaluation period. | Motor power and operating schedule; energy-use estimate; maintenance schedule; parts list; warranty terms; downtime assumptions. | Compare alternatives using the same operating hours, energy price, evaluation period, and cost assumptions. Request the calculation method rather than relying on an unsupported savings claim. |
| Risk assessment and guarding | Check hazards at nip points, drive components, transfers, access points, and areas where people may reach or pass near moving parts. | ISO 12100:2010 provides principles for machinery risk assessment and risk reduction. In the United States, OSHA 29 CFR 1910.212 sets general machine-guarding requirements. | Obtain the risk assessment and guarding layout. Verify that guards, access controls, and safe maintenance procedures address the hazards identified for the actual installation. |
| Safety-related control systems | Confirm the required safety functions, such as guarded-access stopping, and the design level established by the risk assessment. | ISO 13849-1:2023 covers design principles for safety-related parts of control systems; the required performance level depends on the risk assessment. | Request the safety-function specification and supporting validation documentation. Do not assume a particular performance level applies to every conveyor. |
| Electrical equipment | Review electrical design, isolation provisions, control-panel details, wiring documentation, and site supply requirements. | IEC 60204-1:2016, including Amendment 1:2021, addresses electrical equipment of machines. Confirm the applicable edition and local requirements for the installation. | Drawings and equipment documentation identify supply, protection, isolation, and control details; installation acceptance follows the applicable jurisdictional rules. |
| Emergency stop | Verify emergency-stop device locations, accessibility, circuit design, reset behavior, and how the conveyor responds when activated. | ISO 13850:2015 provides principles for the emergency-stop function of machinery. Applicable legal and site requirements must also be checked. | Review the safety design and test the emergency-stop function during commissioning. Resetting the device must not itself restart the conveyor. |
| Applicable standards and jurisdiction | Identify the country of installation and distinguish legal requirements from voluntary engineering standards or contractual specifications. | Written compliance matrix listing each applicable regulation, standard and edition, responsible party, and required evidence. | The purchaser and supplier agree in writing on the applicable requirements before design approval; a standards reference alone is not proof of conformity. |
| Commissioning and acceptance | Define inspections and functional tests for capacity, controls, safety devices, noise or other project-specific requirements. | Commissioning plan; test records; agreed acceptance criteria; outstanding-items list. | Acceptance criteria are measurable and agreed before purchase. Test results and corrective actions are documented before final handover. |
| Spare parts and maintenance | Check which wear parts are used, how they are identified, expected maintenance tasks, and the availability of manuals and replacement parts. | Recommended spare-parts list; maintenance instructions; parts identification; stated availability and lead-time commitments. | Critical parts can be identified and ordered from the documentation; maintenance tasks, intervals, and required skills are stated. |
| Long-term technical support | Clarify support hours, response targets, service coverage, software or controls support, warranty exclusions, and escalation arrangements. | Written support agreement with service scope, contact method, response-time targets, warranty period, and parts-support terms. | Commitments are contractual and suited to the site’s operating schedule. Treat response times and parts availability as supplier commitments, not universal industry guarantees. |
Note: Standards editions and legal requirements can vary by jurisdiction and application. Confirm the current applicable requirements with the responsible safety, engineering, or compliance professional before purchase and installation.