Contract Manufacturing for Injection Molded Plastic Products in North America
(800) 824.0607
Choosing an injection machine is not a matter of buying the largest press your budget allows. The right choice depends on the part, material, mold, and production target. A thin-walled container may need fast injection and precise control. A compact connector may depend more on repeatable shot size and stable clamping. Small details matter.
John Bozzelli, an injection-molding process consultant, is known for emphasizing disciplined process control. A practical paraphrase of that approach is: “Choose the machine around the part and process, not the other way around.” This is a paraphrase, not a verbatim quotation. It captures a useful point: machine specifications only matter when they support the actual molding job.
This guide looks at the key checks behind a sound decision. These include clamping force, shot capacity, injection pressure, tie-bar spacing, mold dimensions, and the material’s processing window. It also considers cycle time, automation, energy use, service support, and room for future production changes. Not just tonnage.
A common mistake is to compare machines by one headline number. That can leave a mold difficult to install, or a shot too close to the machine’s limit. A carefully chosen injection machine should fit today’s part and leave practical operating margin. Still, no checklist replaces trials with the intended mold and resin. Real production can expose assumptions that looked reasonable on paper.
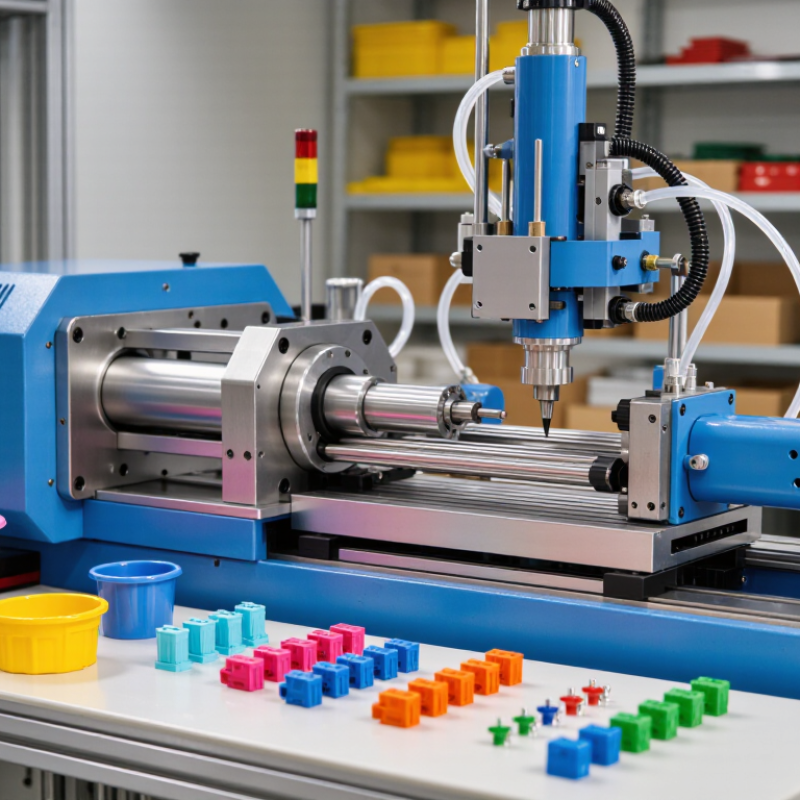
Before comparing injection machines, define the part you need to make. Record its dimensions, weight, wall thickness, projected area, and expected tolerances. Note whether it has deep ribs, inserts, or cosmetic surfaces. These details affect mold design, filling behavior, and the required clamping force. Small parts are not always simple. Thin walls, for example, may need faster filling and tighter process control.
Identify the resin and check its processing requirements. Drying time, melt temperature, and sensitivity to moisture can change cycle time and equipment needs. Then estimate production volume, shift patterns, and acceptable scrap rates. A machine sized only for today’s order may become a bottleneck; one chosen for peak capacity may sit underused. That trade-off deserves a hard look. Compare shot capacity with the actual part-and-runner volume, and check mold dimensions against platen size and tie-bar spacing. Ask about repeatability, maintenance access, and available utilities, too. A spreadsheet can help, but its assumptions may be wrong. Verify estimates with resin data, mold specifications, and trials when possible.
Choosing clamp force starts with projected area, not part weight. Projected area is the part’s silhouette on the mold’s parting line. Include every cavity and the runner system. A common estimate is 2–5 tons per square inch of projected area. For a 20-square-inch footprint, that suggests about 40–100 tons. That is a broad range.
The right point within that range depends on the process. Thin walls, difficult-to-fill features, and higher injection pressure may increase the force needed to prevent flash. Resin behavior, gate location, and mold condition matter too. A simple calculation cannot capture every detail. Use it as a starting estimate, then check the machine’s capacity and the mold’s limits.
Test shots provide useful evidence. Look for flash along the parting line, uneven filling, or signs of excessive clamping. Too little force can let the mold separate; too much may add wear without improving the part. Small adjustments help. I would not treat the 2–5-ton rule as a guaranteed setting. Record the results, adjust carefully, and confirm that parts remain consistent across repeated cycles.
How to Choose the Right Injection Machine?
Size Shot Capacity for the Part and Runner, Not Just the Part Weight
A machine’s shot capacity must cover the complete shot: every cavity, the sprue, and the runner system. A 42-gram part may need a much larger shot when a cold runner feeds several cavities. Ignoring that material can push the injection unit near its limit. That sounds simple. It is often missed.
Plastics Technology’s published machine-sizing guidance describes a common usable-shot range of roughly 20–80% of the barrel’s rated capacity. Treat this as a screening guideline, not a guarantee: ratings may use polystyrene, while production resin can differ in density and flow behavior. Calculate the full shot in the actual resin, then check the machine’s rating basis and leave room for a stable cushion. For example, a large runner can make a seemingly suitable machine too small; an oversized barrel can also make a small shot harder to control. I would recheck the calculation after changing cavity count or runner design.
Tips: Weigh a complete molded shot, including runners, and compare it with the machine’s resin-adjusted capacity. Record cushion and shot consistency during trials. If the part weight looks right but the cushion varies, the sizing decision may need another look.
Illustrative example: four parts at 18 g each (72 g total) plus an 18 g runner produce a 90 g shot. The chart compares that complete shot with candidate machine shot capacities.
Shot utilization = total shot weight ÷ nominal machine shot capacity. Do not size from part weight alone: include runners, and confirm the machine’s material-specific capacity and acceptable operating range with its manufacturer.
A mold may fit the platen but still fail to pass between the tie bars. Measure the mold’s maximum width and height, including clamps, hoses, and any projecting fittings. Compare these dimensions with the machine’s tie-bar spacing. Leave practical clearance for loading and alignment; a paper fit can become awkward on the shop floor.
Tips: Check the machine drawing, not just its sales sheet. Confirm platen dimensions and mounting-hole locations. Make sure the mold thickness falls within the machine’s minimum and maximum mold-height range. Also verify opening stroke and daylight for part removal. Small details matter.
A common oversight is checking only the mold’s outside dimensions. The locating ring, ejector setup, and clamp access can create conflicts after installation. Record actual measurements and compare them with the machine manual or a qualified technician’s review. If the mold sits near a thickness limit, pause and verify the adjustment range. It is easy to assume the clamp unit will accommodate it, and that assumption may be wrong.
Choosing an injection machine begins with matching its screw to the resin, not simply selecting a familiar machine size. A general-purpose screw often uses an 18:1–24:1 L/D ratio, meaning its length is 18 to 24 times its diameter. This range suits many standard thermoplastics and supports steady melting and mixing. It is a starting point, not a guarantee. Small details matter.
Resin behavior can change the choice. A glass-filled material may need wear-resistant components, while a heat-sensitive resin may require gentler processing and shorter residence time. Check the resin supplier’s processing data, then compare it with the screw’s compression ratio, mixing features, and the machine’s shot capacity. During trials, record melt temperature, cycle time, cushion, and visible defects. These measurements help reveal whether the screw is processing the resin consistently. A ratio within the usual range can still perform poorly if the screw geometry or settings are mismatched. That part is easy to overlook.
| Resin or Material Group | Common Screw Approach | Typical L/D Ratio | Design Considerations | Practical Selection Check |
|---|---|---|---|---|
| General-purpose amorphous thermoplastics, such as ABS, PS, and SAN | General-purpose, three-zone screw | 18:1–24:1 | A conventional feed, transition, and metering section is often suitable. Compression and mixing requirements depend on the specific resin grade and color package. | Confirm the screw can melt the shot consistently without excessive residence time or shear heating. |
| Polyolefins, such as polyethylene and polypropylene | General-purpose or polyolefin-oriented three-zone screw | Commonly around 20:1–24:1 | These materials generally process readily, but melt behavior varies by grade. Screw geometry should provide stable melting and adequate output for the cycle. | Check the resin supplier’s processing guidance and verify melt quality at the intended cycle time. |
| Hygroscopic engineering thermoplastics, such as polycarbonate, nylon, and PET | Material-specific screw; barrier or mixing features may be considered where appropriate | Often around 20:1–24:1, depending on resin and machine | Moisture control is critical for many grades. Excessive shear, long residence time, or unsuitable melt temperatures can contribute to degradation. | Prioritize correct drying, residence-time control, and the resin maker’s recommended processing window. |
| Heat-sensitive materials, including PVC compounds | Low-shear, material-specific screw | Varies by compound and machine; avoid selecting by L/D alone | Excessive shear and heat can cause degradation. Screw and barrel design should be selected for the particular PVC formulation and stabilizer system. | Obtain compound-supplier guidance and review temperature control, screw speed, and residence time. |
| Glass-fiber-reinforced thermoplastics | Wear-resistant screw and barrel; mixing design suited to the compound | Often within a conventional range, but application-dependent | Glass fibers are abrasive and can wear screw and barrel surfaces. Screw design should balance dispersion with fiber-length retention and acceptable shear. | Check material compatibility, expected wear, and the required balance between fiber distribution and part performance. |
| Resins containing color concentrates or additives | General-purpose screw with a suitable mixing section, or a dedicated mixing screw | Commonly around 18:1–24:1 | Mixing needs depend on additive type, concentrate level, and base resin. More mixing is not always better if it increases shear or residence time. | Evaluate color or additive uniformity alongside melt temperature, cycle time, and material sensitivity. |
Note: L/D is the screw’s length-to-diameter ratio. The ranges shown are general selection guidance, not universal specifications; actual screw geometry and processing limits should be confirmed with the resin supplier and machine manufacturer.